

Search keywords:
product name, product type, model number,
test method, manufacturer, technique, application
-
Cone Calorimeter
The import of American VTEC, cone calorimeter ultra high cost performance
more
-
Digital Elmendorf Tearing Tester
Pendulum method test material tear strength, operating more simple, more accurate data
more
-
ZwickiLine Materials testing machines
Top of the world's leading universal material testing machine
more
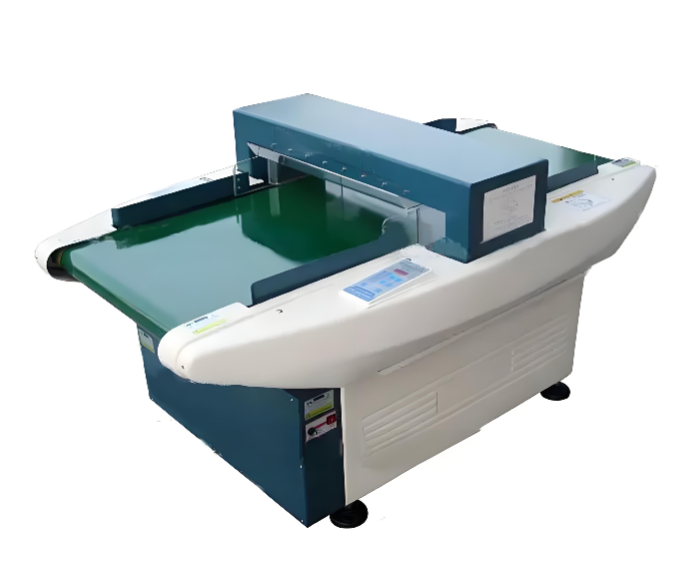
Conveyor needle detector
BACK

Standards:
Applications:
Applicable to shoes, hats, testing,broken needles andiron substances.
Product Information:
The Conveyor Needle Detector is an automated inspection device used to detect metal needle fragments or other metallic contaminants in textiles, garments, and related products during production and packaging processes. It uses a conveyor system to automatically transport products through the detection area, helping ensure product safety, improve quality control, and prevent potential hazards caused by metal contamination.
Basic parameters:
| Item | Specification |
|---|---|
| Power Supply | AC 220 V, 50 Hz ±10% |
| Power | 60 W |
| Detection Width | 600 mm |
| Product Passing Height | 150 mm |
| Sensitivity Adjustment | 0–10 Levels Adjustable |
| Detectability | 1.5 mm Fe Iron Ball Detection |
| Conveyor Belt Speed | 30 m/min |
| Overall Dimensions (L × W × H) | 1600 × Customized × 500 mm |
| Gross Weight | 120 kg |
Function and features:
1.Configure with anti-static non-metal rubber conveyor belt.
2. Alarm modes are respectively sound and light to work simultaneouslv.,enable to help operators to find
3.Machine equipped with counting function, it is divided into aood product. bad product and summation.
4.Possess the detection of thiek fahrin anyd thun facu mnto good proquct, bad product and summaon. oood andautomatic counting etc.
5.The machine adoots soecial mannetio.ogsl 0mtfioall, to makeparticularly high detection accuracVg and coienotihig macerIals and special technology to manuftacture scien licany n needledetector field currently.
FAQs:
1. What is a Conveyor Needle Detector used for?
It is used to detect broken needles, metal fragments, and other metallic contaminants in textile and garment products.
2. How does the machine work?
Products pass through the conveyor detection area, and the system automatically identifies metal objects and triggers an alarm when detected.
3. What are the advantages of a Conveyor Needle Detector?
It provides fast detection, high sensitivity, continuous operation, and helps improve product safety.
4. Which industries can use this equipment?
It is widely used in garment manufacturing, textile production, footwear, luggage, and other industries requiring metal contamination inspection.
5. Can it be integrated into a production line?
Yes. It can be installed in automated production lines for continuous inspection and quality control.